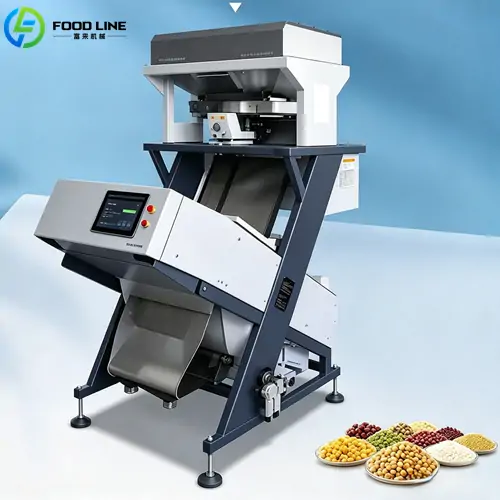
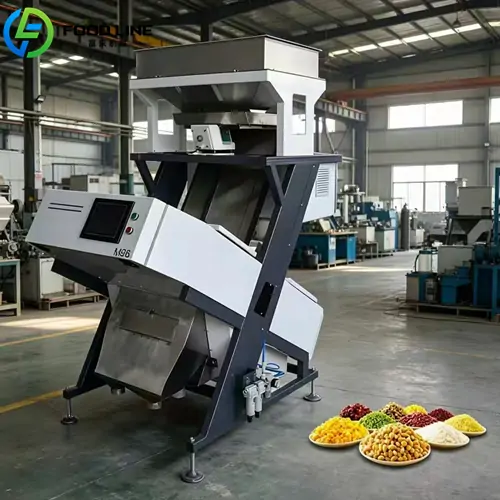
The rice sorting machine uses four Phoenix industrial cameras with a 5,400-pixel camera system. The cameras capture detailed grain images for color analysis. The system helps identify small color differences and visible defects.
Multiple Sorting Modes
Different rice varieties require different sorting standards. The machine supports 6 sorting modes for different defect-removal requirements.
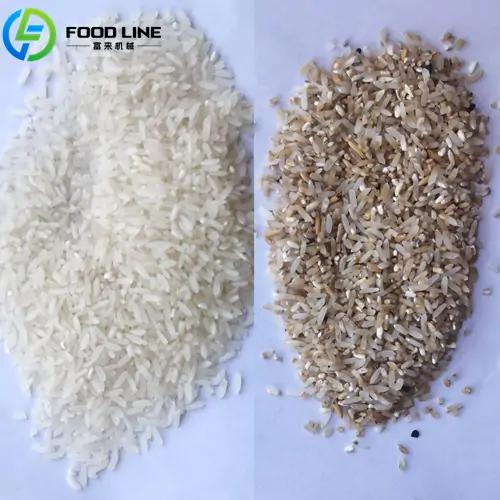
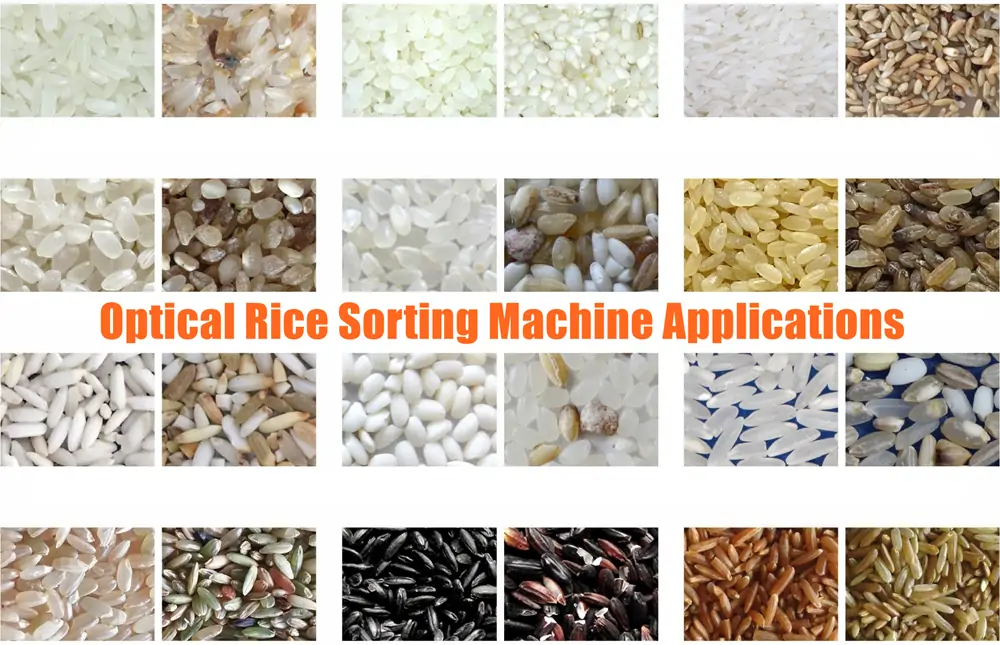
Operators can configure positive or reverse sorting for selected off-color and chalky grains. Combined sorting modes can target yellow, white, and translucent grain differences, subject to the machine’s software configuration.
Intelligent Image Processing
The sorting system analyzes grain color and visual characteristics. Advanced sorting algorithms can help distinguish defective grains from acceptable rice.
High-Speed Air Ejection
The HR2 uses high-frequency air ejectors to remove selected grains. Precise ejection helps separate defective rice while limiting the loss of acceptable grains. Its sorting system is designed for efficient operation and controlled compressed-air consumption.
Easy Touchscreen Operation
The machine features a 12.1-inch touchscreen for operating and adjusting sorting parameters. Operators can select suitable settings and monitor the sorting process through the interface. This mini rice color sorter machine is easy to operate.
The HR2 rice color sorter follows a simple, automated sorting process.
Step 1: Feed the Rice
Rice enters the machine through the feeding system. A vibrating feeder distributes the grains evenly across the sorting channels.
Step 2: Capture Grain Images
Four Phoenix industrial cameras capture detailed images of the rice. The image acquisition system identifies color differences and visible defects.
Step 3: Analyze and Identify Defects
The sorting software compares grain characteristics against preset standards. It identifies unwanted grains, including yellow, chalky, and discolored rice.
Step 4: Remove Defective Grains
The control system activates the corresponding air ejectors. Compressed air removes selected grains from the main product stream.
Step 5: Collect Sorted Rice
The machine separates the accepted rice from the rejected material. Operators can adjust sorting parameters to meet different quality requirements.